How to Handle Cheese Products on Conveyors
What's the best type of conveyor equipment for cheese processes?
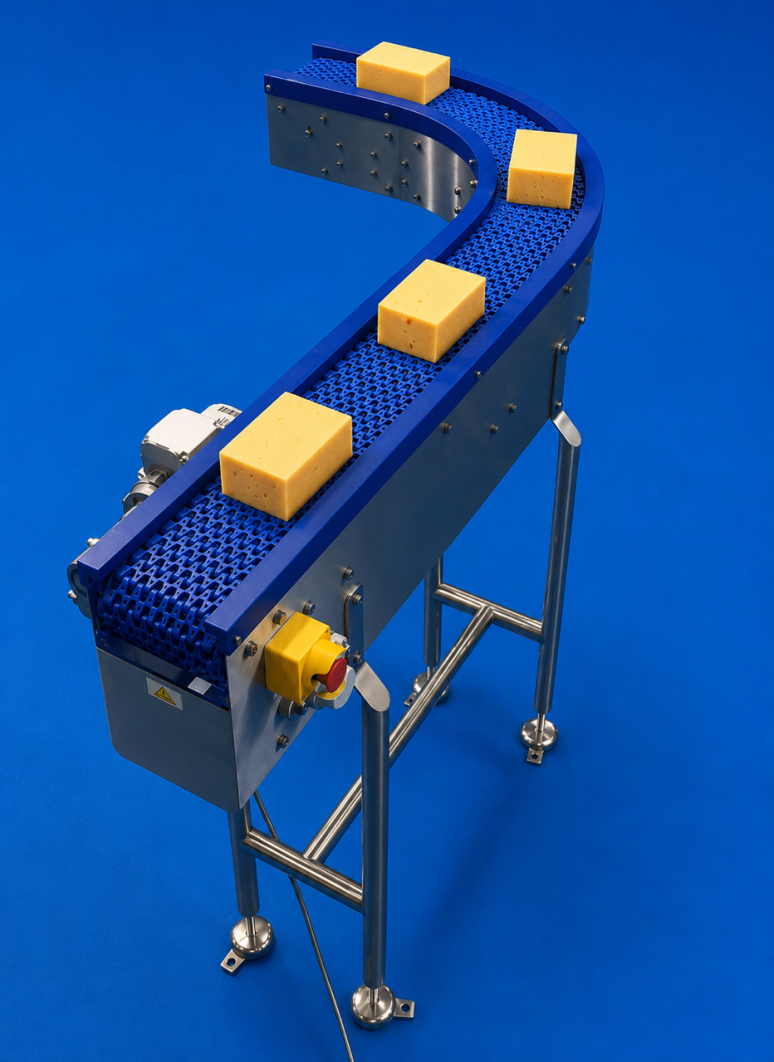
The type of conveyor equipment required for cheese processing will depend heavily on the specific application, the condition of the cheese product, and the environmental demands of the production line. Cheese manufacturing involves a wide range of processes including cutting, slicing, grating, cooling, waxing, packaging, and transportation of finished products, and each stage places different demands on conveyor systems. For this reason, selecting the correct conveyor is essential not only for operational efficiency but also for maintaining hygiene standards, product quality, and food safety compliance.
Conveyor Handling Grated Cheese
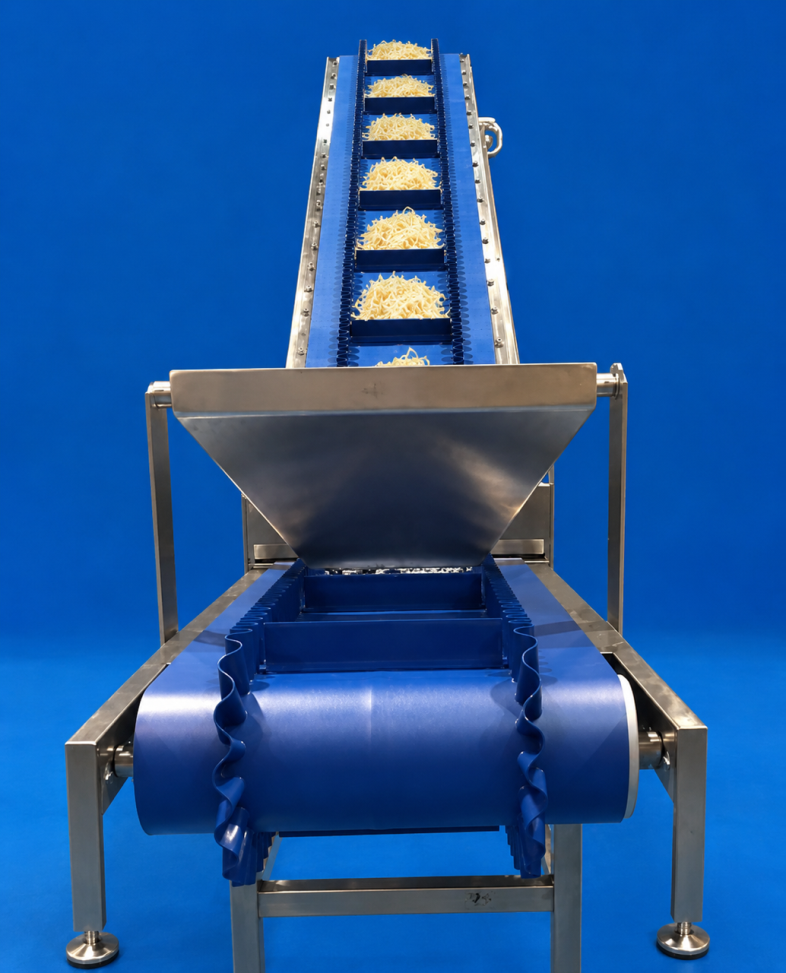
This application was loaded grated cheese in hopper onto a flighted side wall belt with cleats to elevate the cheese to a higher level and discharge through a chute where it was then conveyed to the packing area.

Cheese Handling on Silicone Belt
This application was handling waxed cheese on a food grade silicone belt to help with non stick properties.
Modular Belt Wax Cheese
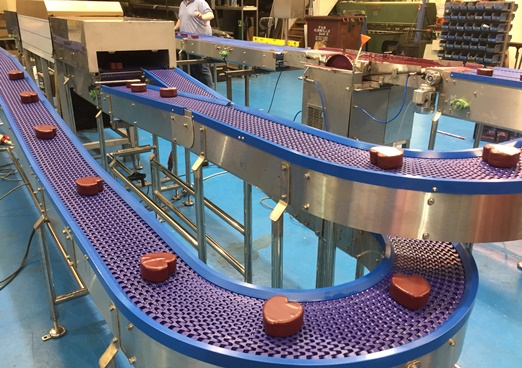
This application was a repeat customer that required raw cheese to be dipped in an enrober to case with wax then transported on a modular belt conveyor to a cooler which on exit flipped the half coated cheese and repeated the process to coat both sides with wax.
Processes involving temperature extremes require more specialised conveyor solutions. For example, wax enrobing applications typically involve elevated temperatures where standard food-grade belts may not perform effectively. In these cases, high-temperature resistant belts, silicone belts, or stainless steel wire mesh conveyors are commonly used. Wire mesh belts are particularly effective because they can tolerate heat exposure while also allowing airflow to assist with cooling the wax-coated cheese after the application process. Cooling tunnels and drying systems similarly benefit from open mesh or wire belt designs that encourage airflow and moisture drainage.
Creamery Cheese Factory
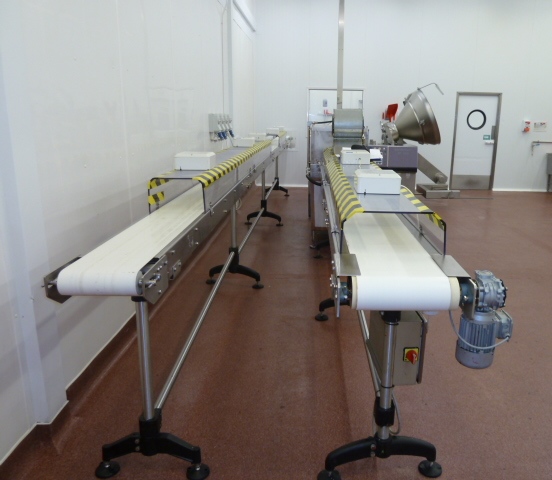
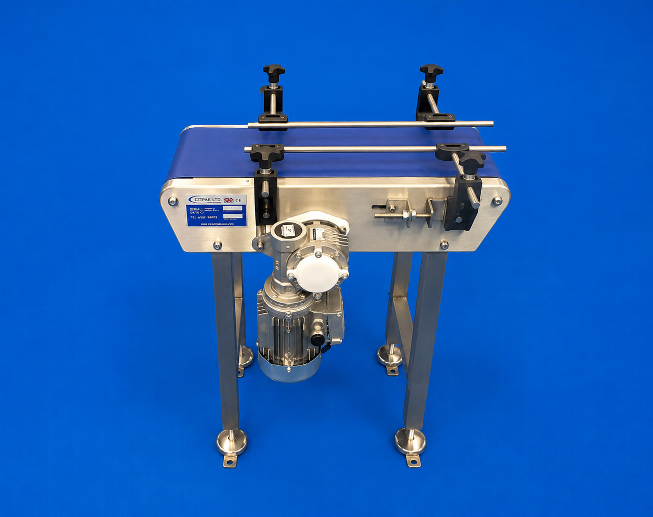
This application was for cream cheese factory with 2 white belt food grade conveyors with a perspex cover.
90° Transfer for Cheese

Cheese Transfer with Swipe arm to move cheese to another conveyor for processing.

Twin Side Belt Transfers
Automated twin grip belts can be used to transfer cheese for either labeling, coding, printing or inspection.

And lastly you can use rotary tables this application dropped cheese from the belt conveyor onto the lazy suzan for hand unloading.
Pick and Pack Cheese Conveyor
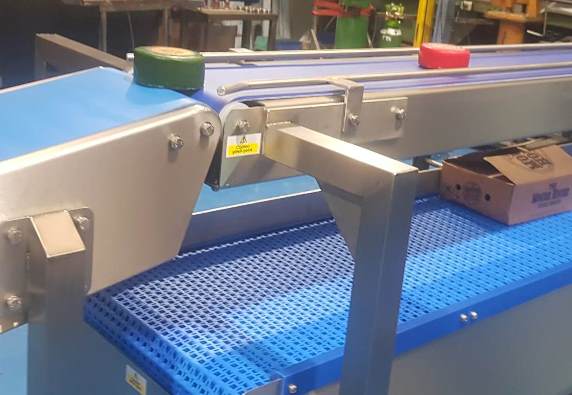
Different cheese products also require different conveyor belt characteristics. Soft cheeses, shredded cheese, and grated products often benefit from non-stick belt surfaces that reduce product build-up and improve transfer efficiency. Inclined conveyors transporting grated or shredded cheese may require sidewalls or flights to prevent rollback and spillage during production. In contrast, heavier cheese blocks or packaged products may be better suited to chain conveyors or modular plastic systems capable of handling increased product weight. |